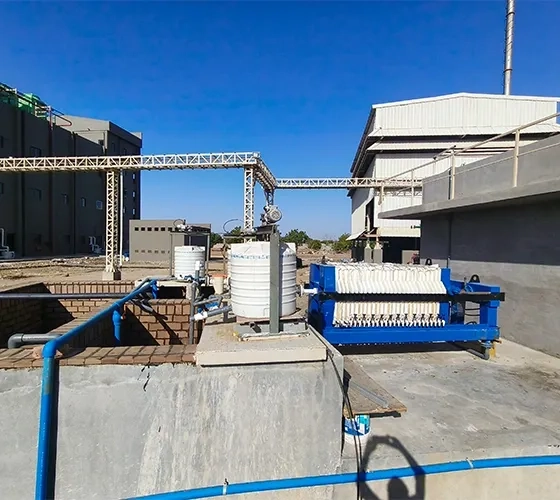
Our dedicated manufacturing blocks feature specialized zones for intermediate and API production, designed with unidirectional flow to ensure product integrity and cGMP compliance.
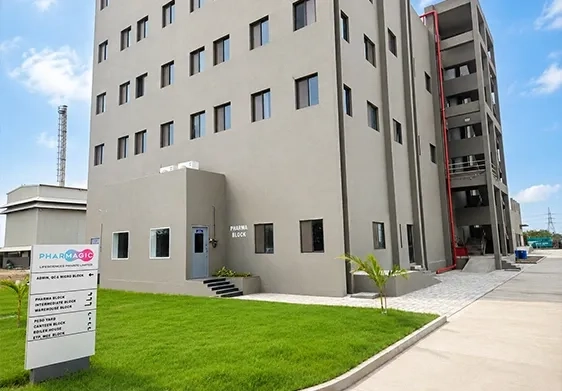
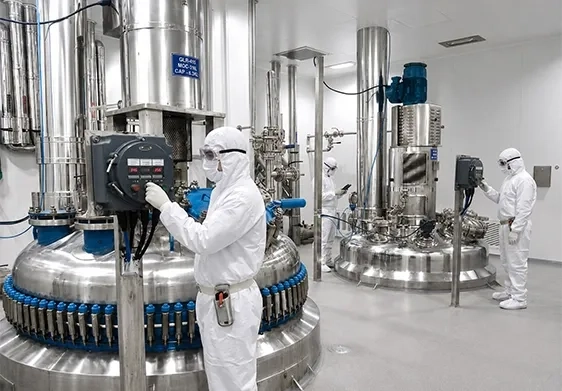
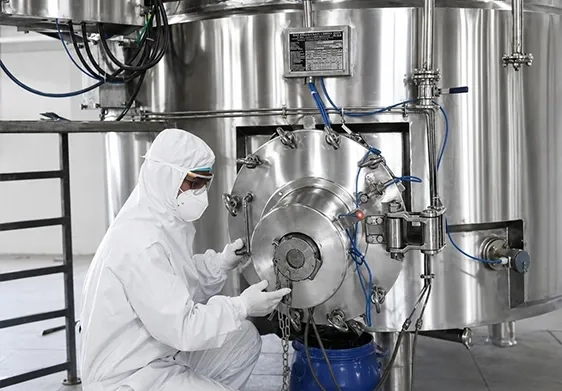
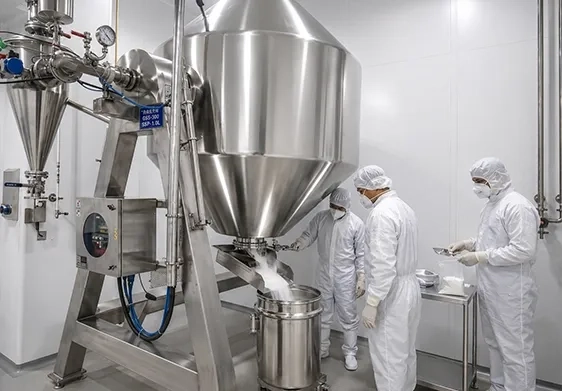
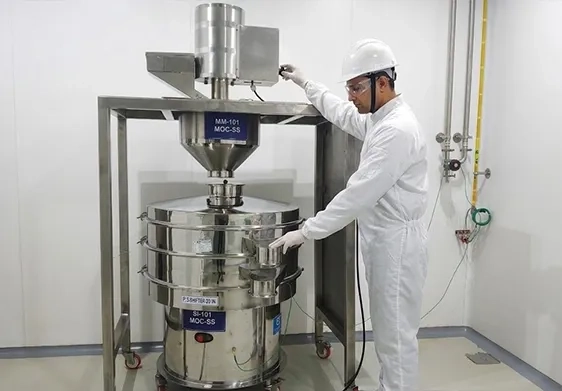
Our advanced manufacturing infrastructure comprises dedicated blocks for API production and intermediates, designed with unidirectional flow to ensure product integrity and cGMP compliance.
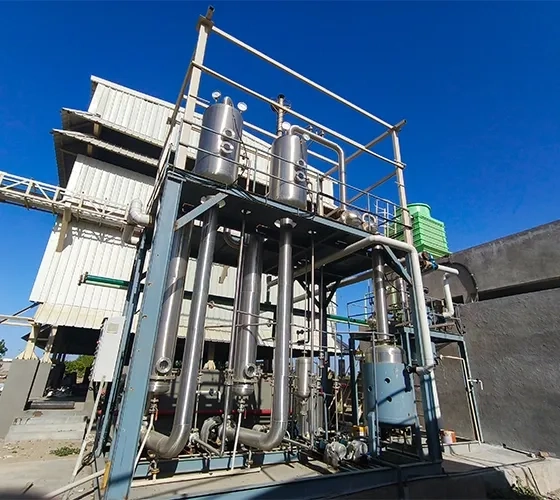
Equipped with SS 316L and glass-lined reactors, the facility supports a wide range of chemical processes including condensation, distillation, crystallization, acetylation, and oxidation.
Integrated filtration and drying systems such as centrifuges, ANFD, and RCVD, along with closed material handling, ensure contamination control. Finishing operations include precision milling, sifting, and blending in dedicated areas. The facility operates within ISO Class 8 clean rooms, featuring separate AHUs, PU flooring, and strict environmental and personnel flow controls to maintain consistent quality.
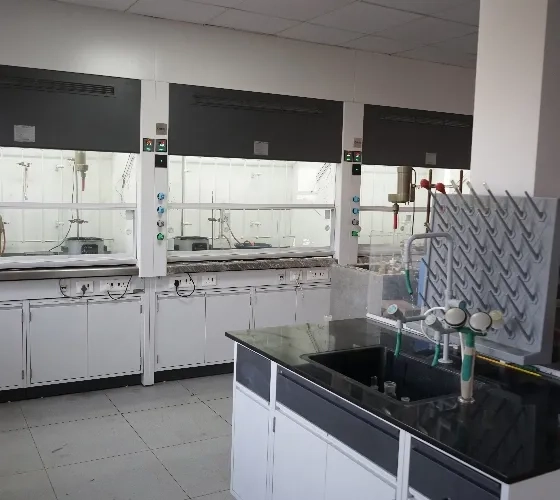
Our R&D center focuses on developing cost-effective, non-infringing, and scalable processes for complex APIs, driving innovation from lab to commercialization.
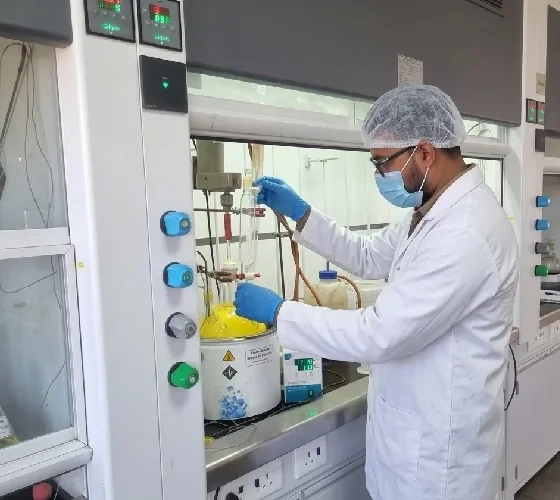
Our R&D center is committed to advancing innovation by developing cost-effective, non-infringing, and scalable processes for complex APIs, ensuring smooth transition from laboratory research to full-scale commercialization. With expertise in API process development, we design and optimize synthetic routes that enhance yield, promote solvent recovery, and follow green chemistry principles.
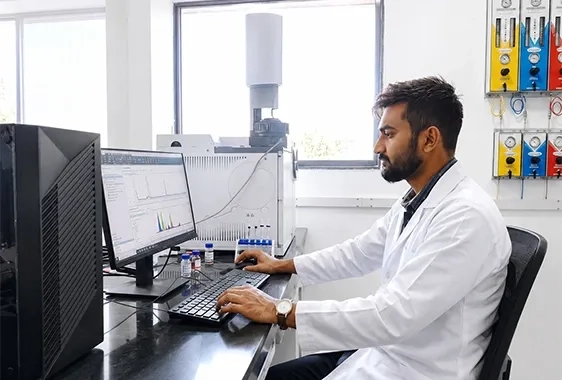
Robust analytical methods such as HPLC and GC are developed and validated in line with ICH guidelines to guarantee quality across raw materials, intermediates, and finished products. We specialize in seamless process scale-up and technology transfer from Kilo Lab to commercial manufacturing, maintaining reproducibility and safety at scale.
Through Quality by Design (QbD), we embed product quality into every stage using systematic approaches and risk management. Additionally, our team provides comprehensive regulatory support, including technical data packages for DMF filings, impurity profiling, and effective responses to regulatory queries, ensuring compliance and smooth approvals.


Our facility operates on a backbone of advanced utility systems designed for 24/7 reliability, environmental sustainability, and strict adherence to pharmaceutical water and air quality standards.
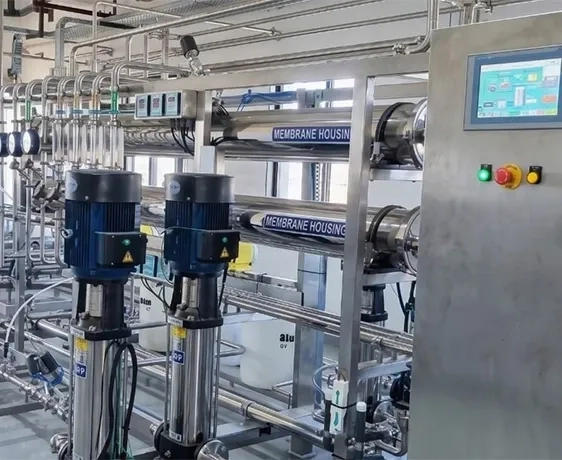
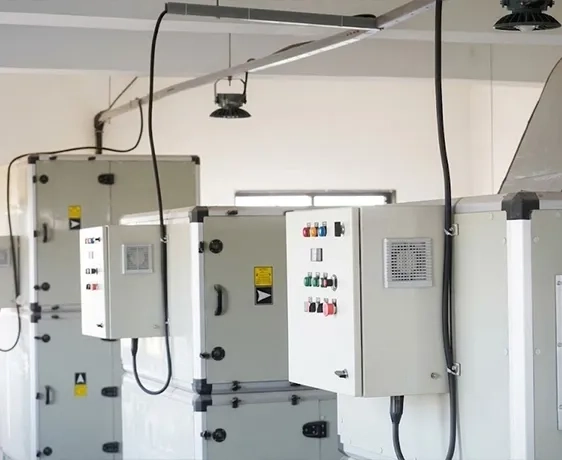
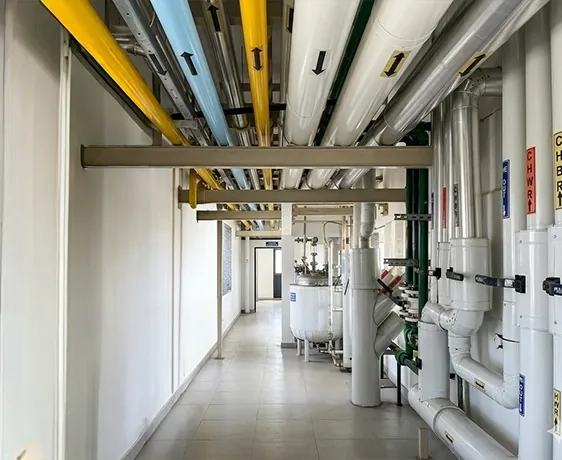
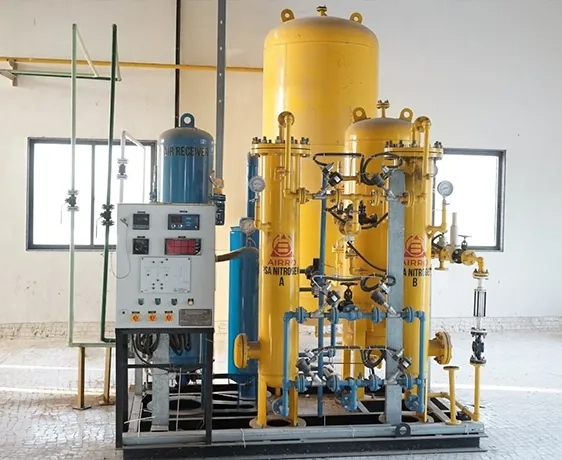
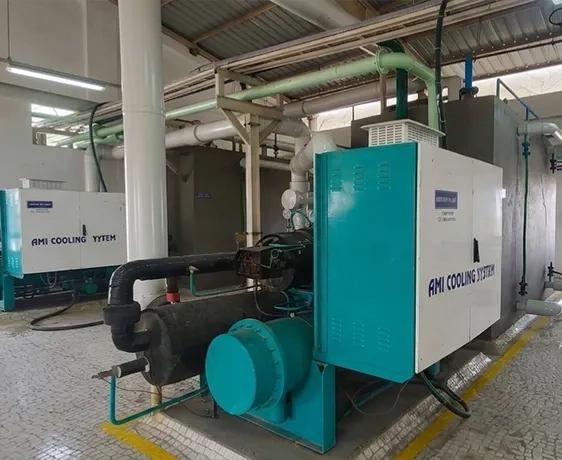
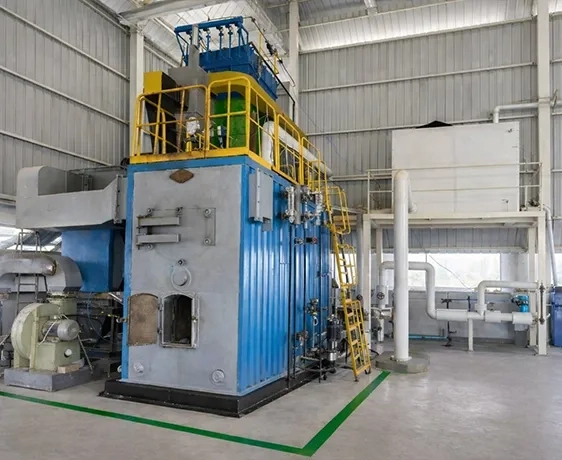
Our facility is supported by advanced utility and support systems that ensure round-the-clock reliability, environmental sustainability, and strict compliance with pharmaceutical water and air quality standards. The purified water system features double-pass RO with EDI units, stainless steel continuous loops, UV treatment, and dosing systems to consistently meet USP/IP standards.
Independent AHUs with terminal HEPA filtration maintain controlled temperature, humidity, and pressure across critical areas, achieving ISO Class 8 conditions. Power and steam requirements are met through a high-efficiency boiler shed, uninterrupted backup via DG sets, and dedicated UPS for critical controls, all overseen by a 24/7 engineering team. Environmental Health & Safety (EHS) measures include zero liquid discharge systems, advanced fire safety infrastructure, and continuous environmental compliance monitoring, ensuring both operational excellence and sustainability.
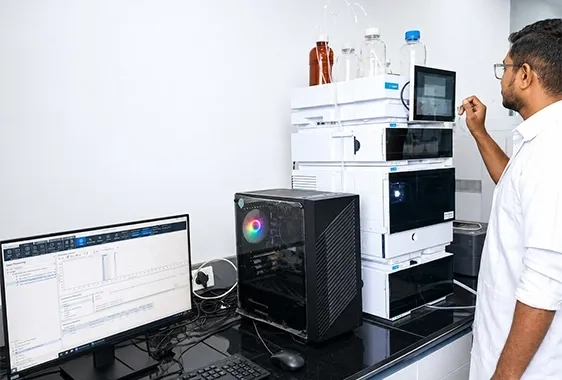
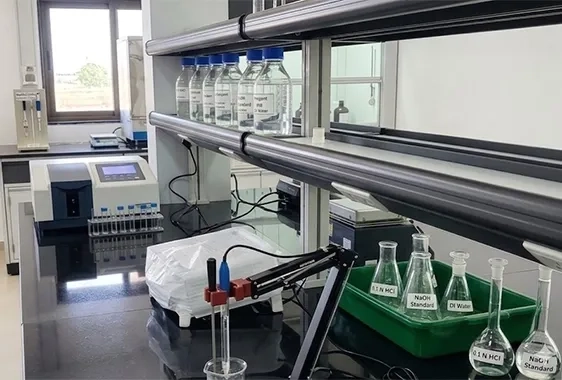
Our quality control facilities are physically separated from production areas, ensuring complete independence, data integrity, and rigorous testing standards according to cGMP/GLP norms.
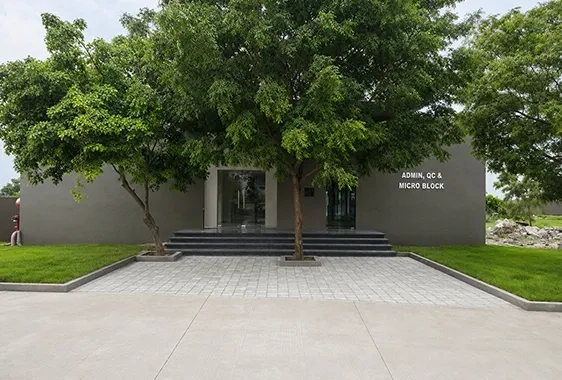
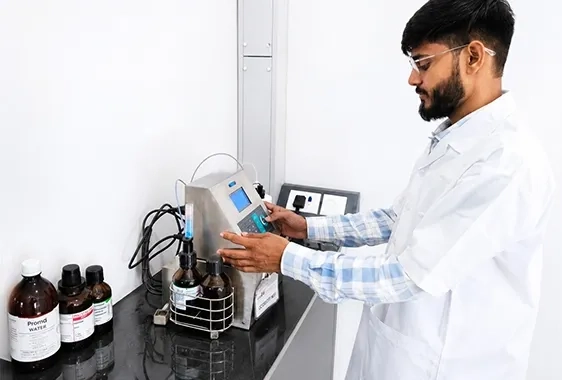
Our QA & QC laboratories are designed to operate independently from production areas, ensuring complete data integrity and compliance with cGMP and GLP standards. The Quality Assurance (QA) unit manages QMS, document control, batch review, release, and deviation handling, while the QC Chemical Lab conducts wet chemical analysis, precision weighing, and advanced instrumental testing with HPLC and GC systems for raw materials and finished goods.
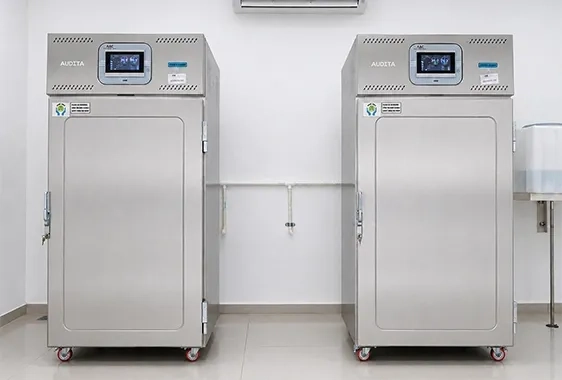
The Microbiology Lab is equipped with dedicated HVAC systems, power backup, and facilities for sterility testing, environmental monitoring, and stability studies under ICH guidelines. To safeguard sample integrity, controlled temperature zones, biometric access, and retention sample rooms are maintained, providing a secure and reliable environment for long-term storage and regulatory compliance.


Our warehousing operations ensure strict material segregation and preservation through controlled environments, fully compliant with cGMP storage guidelines.
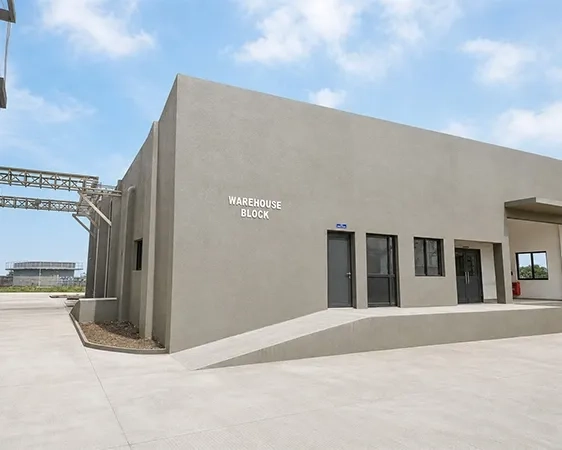
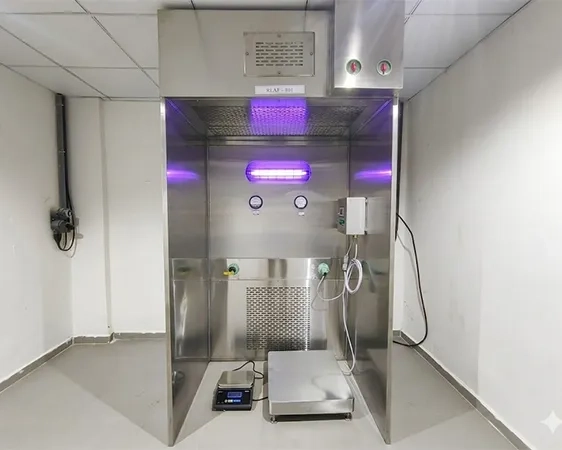
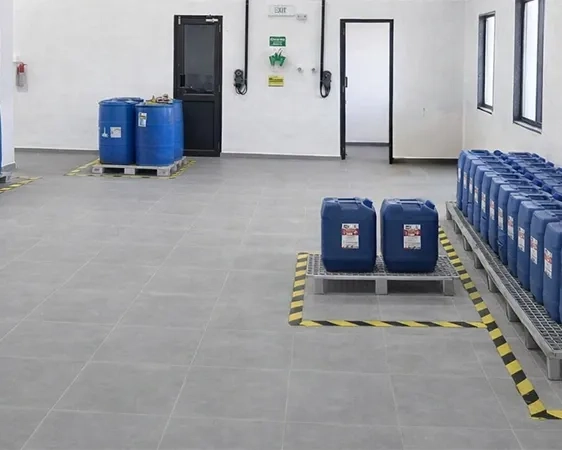
Our Warehouse & Storage Infrastructure is built to ensure strict segregation, preservation, and compliance with cGMP storage guidelines, providing a safe and controlled environment for raw materials, intermediates, and finished goods.
Dedicated zones are maintained for APIs, solvents, packaging materials, and finished products, supported by clear status labeling systems such as quarantine, approved, and rejected. High-density racking, palletized storage, and bonded storage rooms enhance efficiency and safety, while refrigeration units safeguard sensitive items.
Continuous temperature and humidity mapping, 24/7 environmental monitoring, and alarm systems guarantee optimal conditions. To prevent contamination, dispensing and sampling are conducted in designated RLAF booths with controlled access protocols, ensuring precision, safety, and regulatory compliance across all warehousing operations.
We are dedicated to sustainable manufacturing practices, integrating advanced environmental controls and safety protocols to protect our ecosystem and workforce.
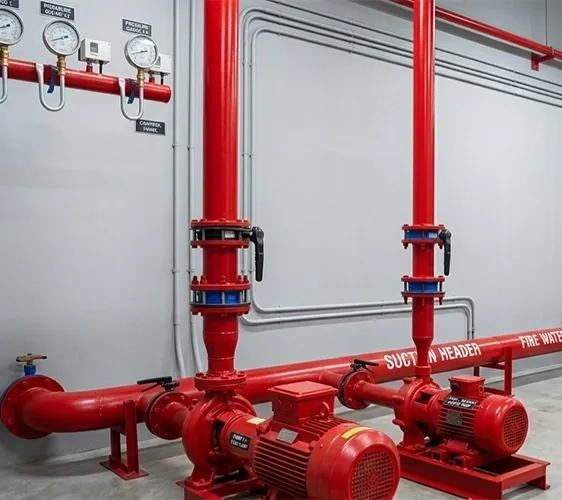
Our EHS & Safety Standards framework is designed to safeguard both employees and the environment through rigorous protocols, advanced protective equipment, and continuous monitoring. Personal protective equipment is mandated according to zone-specific risks, including gloves, goggles, respirators, chemical-resistant aprons, and anti-static footwear.
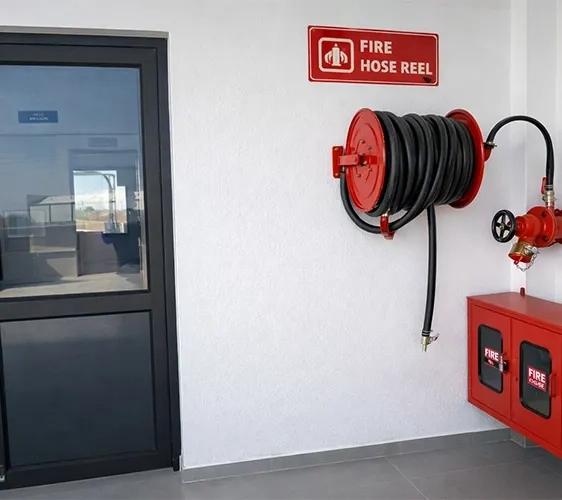
Fire safety is ensured with comprehensive hydrant and sprinkler systems, regular maintenance, and emergency evacuation drills. Environmental safety is prioritized through a “Green Belt” policy, zero liquid discharge systems, and advanced wastewater treatment. Hazardous materials are managed under strict SOPs with segregated storage, spill control kits, and MSDS availability at all usage points.
Employee health is protected through pre-employment and annual medical exams, spirometry and hematology profiling, and ongoing occupational health checks. Finally, emergency response readiness is maintained with defined protocols, regular mock drills, on-site first aid, and rapid intervention capabilities, establishing a robust safety culture across the facility.